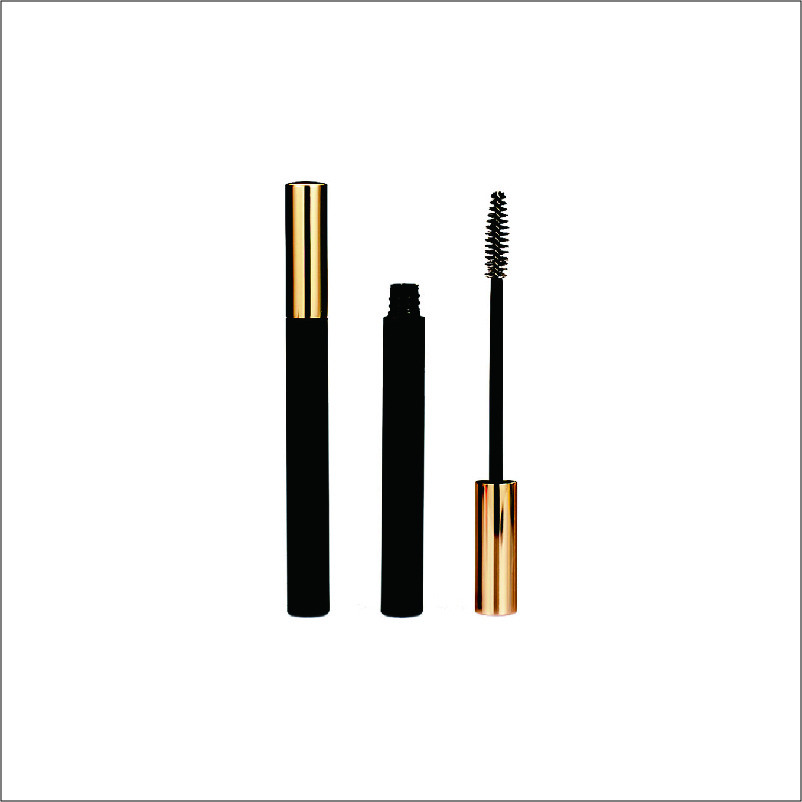
Opening Scene, Hard Numbers, One Big Why
What does a small delay teach a brand about time and trust? In the race to secure empty mascara tubes wholesale, the floor hums, cartons stack, and a deadline breathes down your neck (thik ache, we have all been there). Last quarter, one mid-tier beauty house saw a 14% slip in first-fill due to cap-wiper mismatch; another flagged a 2.2% leak rate tied to inconsistent torque. If speed is the drum, quality is the melody—and both must stay in tune. So, why do teams still chase unit price more than lifecycle cost, even when returns eat margin? Let us walk into the heart of the problem and ask a quieter question: what do we measure, and what do we ignore? Come, we move to the next layer now.
Hidden Friction: Where Procurement Specs Go Thin
To cut through fog, start with the right partner. An empty mascara tube supplier should translate design into repeatable realities. Yet, traditional sourcing often treats tubes as “simple components.” They are not. Real performance lives in the micro-fit between stem and wiper, the torque range of the cap, and the ink’s grip after hot-fill. When teams only chase MOQs and lead time, they skip the tests that matter: wiper tolerances under thermal cycling, torque testing after transit vibration, and silkscreen adhesion over UV aging. Injection molding can be precise; still, resin grade drift or recycled blend ratios can shift viscosity behavior at the wand—small changes, big mess. Look, it’s simpler than you think: measure what drives the swipe, not just what fills the spec sheet.
Legacy processes also hide costs in downstream chaos. A price win at PO can become a claims storm later—funny how that works, right? Consider first-fill yields, line speed on automated cappers, and reject rates at visual inspection. A tube that passes calipers may still spit micro-leaks when altitude changes hit pallets. And decoration? If silkscreen opacity varies, your black SKU becomes three shades in retail light. The cure is dull but wise: functional tests over nominal checks, including wipe-off stability, drop tests, and cap compression set. When procurement aligns QA with marketing promises, the story holds. When not, it frays in transit, in unboxing, in returns.
Why do good intents fail?
Because teams accept drawings as truth and forget process variation. Because the lab test is clean, and the truck ride is not.
Comparative Insight: Old Playbook vs New Principles
Older playbooks compare quotes; newer ones compare systems. A capable mascara tube manufacturer now uses data loops that bind design, tooling, and logistics in near-real time. The new principle is simple: make the invisible measurable. Inline vision systems track flash and gate vestige. Digital torque cells log every cap close on pilot runs. Resin genealogy tags tie PCR ratios to batch performance—no guessing. Even small factories can deploy low-cost sensors to watch dwell times and cooling curves, then predict warpage. Semi-formal as it sounds, this is not moon-talk; it is shop-floor pragmatism. And when results stream into a shared dashboard, procurement stops arguing about anecdotes and starts comparing distributions—who holds tolerance on Mondays as well as Fridays.
What shifts in practice is choice. Instead of picking the cheapest tube, teams choose the most stable process window. You get fewer leaks, faster line ramp, steadier black-ink opacity. You also see risk earlier: if wiper durometer creeps, the model blinks before the market does—funny how that works, right? Comparative insight means ranking suppliers by functional yield, not only unit price. It means scoring decoration by rub resistance after hot room, not only Pantone claims. In that light, the “best” vendor is the one who keeps your swipe feel consistent from pre-launch samples to the 50,000th piece. Small poetry in a practical world.
What’s Next
We can sum it cleanly. Traditional fixes chase drawings; resilient systems test reality. The lesson: measure function at the interface—wand, wiper, and cap—and you protect both brand promise and margin. From here, an advisory close. Three metrics decide wisely: 1) Functional yield across pilot and first mass run, including torque and wipe tests under thermal cycling. 2) Process capability (Cp/Cpk) on critical dimensions, with traceable resin lots and documented cool time. 3) Post-transit stability: leak rate, decoration abrasion, and cap compression set after vibration and altitude exposure. Choose on these, and the noise falls away. For the record, steady partners keep your story intact, from line changeover to shelf light. And that is how a small part carries big trust—day after day. NAVI Packaging