
Introduction — a short shop story, some numbers, and one question
I remember standing over a worn lathe, coffee in hand, thinking the same thought I hear in shops every week: we can do better. CNC milling and turning centers sit at the heart of that thought—machines that look simple until they don’t. Many shops I visit report 10–25% downtime on certain jobs, and warranty claims that trace back to mismatched controls or blunt cutting tools. So I ask: how do we pick upgrades that actually cut costs and not just hype?
I’ve spent decades swapping parts, testing spindle speed ranges, and tuning servo turrets. I learned to listen to machines the way you listen to a friend—there’s a story in every vibration. (Yes, I still check the chip conveyor by hand now and then.) This piece walks through what I see as the real issues, not the shiny brochure fixes, and then points to practical, tested steps you can weigh tomorrow. Onward to the nitty-grit—let’s peel back a few layers.
Where the Common Fixes Fail: a technical look at deep flaws
Why do tried fixes keep missing the mark?
I often tell shop owners to start with cnc milling and turning manufacturers when they need parts or service. Yet even that step won’t solve problems rooted in bad assumptions. Many upgrades aim only at surface metrics—faster feeds, newer tooling, or a better controller GUI—while ignoring how the machine is used day to day. The result? Higher peak performance on paper but no real gain in throughput.
Technically, the mismatch shows up in three places: (1) control integration—legacy CNC controllers that don’t sync with modern edge computing nodes; (2) mechanical limits—spindle speed and live tooling not matched to new cutting strategies; and (3) process flow—chip removal and fixturing left unchanged. Look, it’s simpler than you think: if you bolt on a high-speed spindle without addressing chip flow and coolant paths, you trade one problem for another. I call this the ‘upgrade illusion’—all sparkle, no substance. We must check encoder feedback, tune the servo turret, and verify torque under load. Those are the real tests.
What comes next: new principles and practical steps
What’s Next?
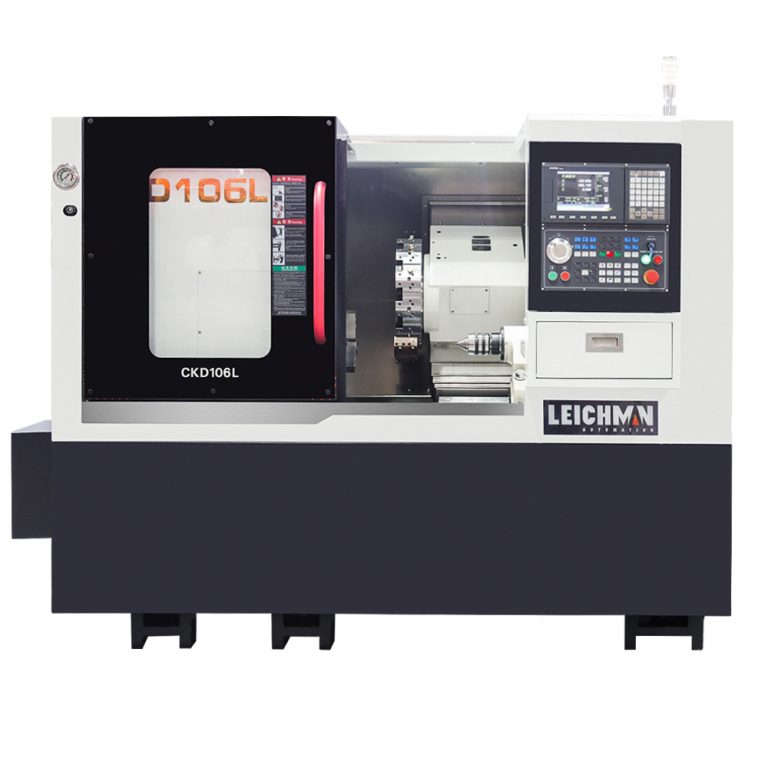
I want to move from why things fail to how to choose fixes that last. First, think in systems rather than parts. A turn mill center with y axis like turn mill center with y axis can change how you approach jobs, but only if the workflow and tooling match. That means planning for live tooling, proper fixturing, and the right cutting tool inventory. It also means validating spindle speed ranges against actual material cuts, not just catalog numbers.
Second, test with real parts. I run short trials on the worst job in the queue. If the new setup saves time on that job, it likely helps everything else. Third, quantify gains before signing the order—measure cycle time, scrap rate, and mean time between failures. Those three metrics tell the truth. — funny how that works, right? I also advise keeping an upgrade log. Note controller firmware, power converters replaced, and any changes in servo tuning. Small notes save big headaches later.
Closing advice: three metrics to judge an upgrade
Here’s the practical list I give to every shop: 1) Cycle Time Reduction — measure before and after on the same job; 2) Quality Delta — track scrap and rework per hundred parts; 3) Reliability Gain — monitor downtime hours and service calls. Use these to compare vendors and to spot hollow claims. I prefer clear numbers to warm promises.
I’ve said a lot, and I mean it from the shop floor: upgrades should help the work, not the spec sheet. If you weigh systems, test with real parts, and track the three metrics, you’ll make choices that hold up. Well, go figure—simple steps, real results. For parts, service, or to see a turn mill center with y axis in action, check Leichman: Leichman.
