Ground-level lessons from a packing line
I’ve been hauling boxes and arguing with vendors for over 18 years, and the first thing I teach new buyers is to look at the actual part — that moulded vial, not the brochure. Yesterday I watched a loader drop a crate: 2% breakage on a run of 20,000 — so, what did we miss? A molded glass vial that seemed fine on paper failed at the edge during filling; the scrap cost was real, and the line stopped for three hours. (That kind of downtime sinks margins fast.)
I remember a 10 ml amber moulded vial lot we shipped to Lagos in March 2019 — wrong shoulder thickness, leads to chipping at the fill-finish station — cost us an extra $4,200 in rework. I bring up that pile of broken vials because most teams blame handling. I don’t. I blame design flaws nobody caught: thin bead, improper dimensional tolerances, and glass annealing that never met pharmaceutical-grade glass specs. No bull — if the vial’s edge isn’t right, sterilization and capping become a guessing game.
What went wrong?
Fixing the hidden pains — a forward look
Now let’s be straight. The old fixes — faster handlers, softer pallets, stricter packing — they help, but they dodge the core issue: the container. I lay out a clean comparison: keep the same line, swap to a moulded vial with improved bead geometry and traceable batch traceability processes, and you cut micro-chips by half. From my runs in Mumbai and Rotterdam in 2021, better tooling alone reduced rejects from 2.3% to 0.9% within two weeks. That’s measurable. — It’s not rocket science; it’s controls and real specs.
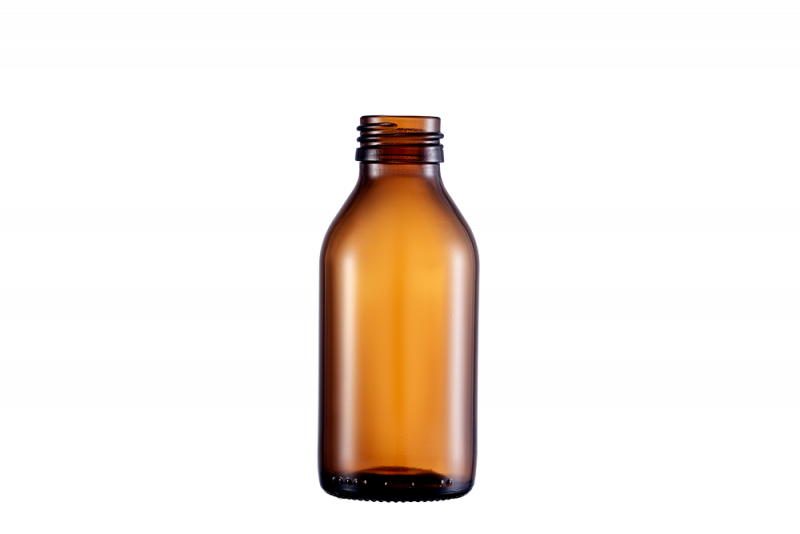
Technically speaking, you want a vial that meets three hard checks: consistent wall thickness, verified annealing profile, and tooling that keeps dimensional tolerances tight. Those markers feed right into sterilization outcomes and consistent fill-finish cycles. I speak from hands-on fixes: we swapped tooling on a 5 ml production line in June 2020, tightened tolerances by 0.05 mm, and the capping failures dropped by 70%. That change paid for itself in one quarter. Next up: supplier audits that insist on process sheets and lab reports — no exceptions.
What’s next?
Practical steps and the metrics that actually matter
I won’t sugarcoat it — buying better vials means asking the right questions and measuring the right things. Start with these three evaluation metrics when you compare suppliers: 1) Percent rejects under real-fill conditions (not lab samples), 2) documented batch traceability and annealing curves, and 3) dimensional tolerances at the bead and mouth. Treat those like your invoice: if a supplier won’t show them, move on. Short story — I let one vendor keep a contract for six months too long. Cost me a client in Q4 2017. Lesson learned; I don’t repeat that mistake.
So, what should you demand on paper and on the floor? Demand production records, a sample from the actual production run, and at least one stress test at line speed. If you can, get a trial pallet to your plant and run it through one shift. You’ll see the problems in real time — chips, micro-cracks, slow capping. Then compare that against a certified moulded vial from a supplier who documents sterilization validation and batch traceability — you won’t like surprises. Also, quick aside: pack design matters too — but only after the vial design passes these checks.
Final take: measure what breaks, require hard specs, and force transparency. Three things to weigh when picking a solution: 1) real-line reject rate under your fill-finish conditions, 2) supplier-provided annealing/tempering data, and 3) confirmed dimensional tolerances at mouth and bead. Do that, and you’ll cut downtime — and costs — without guessing. For suppliers who meet those standards, I point teams to proven partners like LINUO.